
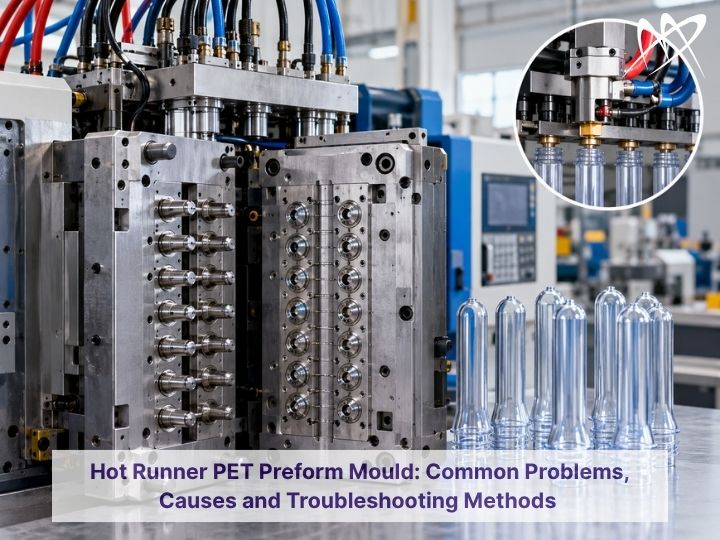
Most production issues on a hot runner PET preform mould don't appear out of nowhere. They build gradually a slight increase in reject rate, a cavity that's consistently a little underweight, a preform that occasionally comes out hazy until the pattern becomes obvious enough to investigate. By that point, tracing the problem back to its actual cause takes longer than it would have if the early signs had been caught at the trial or inspection stage.
PET preform production is less forgiving of hot runner inconsistency than many other injection moulding applications, mainly because PET is sensitive to both temperature and residence time in ways that show up directly as visible defects. A hot runner system running slightly outside its intended parameters can still technically produce parts, just not parts that meet the clarity, weight, or dimensional consistency PET preform applications typically require.
Why Hot Runner PET Preform Moulds Are Prone to Specific Issues
PET preform injection moulding places more demands on a hot runner system than general-purpose injection moulding does. PET requires precise temperature control to avoid thermal degradation, consistent residence time to limit acetaldehyde generation, and even flow balance across every cavity to maintain consistent wall thickness and clarity. Many of the issues covered in this article trace back to decisions made at the hot runner system components selection stage, rather than developing purely from wear or process drift.
A hot runner mould built and tuned for a more thermally stable resin can tolerate minor inconsistencies that would show up immediately on a PET preform mould as haze, weight variation, or surface defects. This is part of why troubleshooting a hot runner PET preform mould often requires checking individual cavity performance rather than evaluating the mould as a single unit a problem affecting one zone of the manifold can look like a process issue when it's actually isolated to a specific flow path.
For manufacturers evaluating a new system, these considerations are particularly important when selecting hot runner PET preform moulds, where cavity balance, temperature uniformity, gate performance, and cooling need to work together.
What to Look for in a PET Preform Mould Manufacturer
When recurring hot runner problems continue despite process adjustments, the mould design and manufacturing approach should also be reviewed. A reliable PET preform mould manufacturer should consider manifold flow balance, temperature control, cooling integration, cavity-to-cavity consistency, gate performance, and component serviceability during the design stage.
For high-cavitation PET preform moulds, these factors become especially important because a small difference in one flow path can create repeated variation in preform weight, clarity, or wall thickness. Reviewing the mould design, trial results, cooling performance, and hot runner parameters together can help identify whether a production issue is process-related or built into the mould system.
Common Problem: Inconsistent Preform Weight Across Cavities
Preforms from different cavities in the same shot coming out at noticeably different weights usually points to a flow balance issue within the manifold, rather than a process setting problem.
Likely causes: An unbalanced manifold design, where flow paths to different cavities aren't geometrically equivalent, is the most common underlying cause. Partial blockage in one nozzle or gate area, or a thermocouple reading inaccurately and causing one zone to run cooler than intended, can also produce this pattern.
Troubleshooting approach: Check cavity weights individually across several consecutive shots to confirm the inconsistency is repeatable rather than random. If the same cavities are consistently light or heavy, inspect flow balance in the manifold and verify thermocouple accuracy in the affected zones before adjusting process settings, since adjusting pressure or temperature to compensate for a hardware imbalance typically creates new problems elsewhere. This kind of cavity-to-cavity imbalance is exactly what mould trial and validation is meant to catch before a mould ever reaches full production.
Common Problem: Stringing or Drooling at the Gate
Resin stringing or drooling from the nozzle tip between cycles typically indicates the gate isn't freezing off cleanly, which is a common issue in hot runner systems running thermal-gated nozzles rather than valve-gated designs.
Likely causes: Nozzle tip temperature running slightly too high, insufficient decompression after injection, or a worn nozzle tip no longer sealing as designed are the most frequent causes.
Troubleshooting approach: Verify actual nozzle tip temperature against the target setting, since this is an area where thermocouple placement errors commonly cause a discrepancy between displayed and actual temperature. Inspect the nozzle tip for wear if temperature is confirmed accurate, since a worn tip may need replacement rather than a process adjustment.
Common Problem: Haze or Clarity Issues in Finished Preforms
Haziness in a PET preform, particularly concentrated in specific areas rather than distributed evenly, usually traces back to inconsistent cooling or excessive residence time in the hot runner system rather than a cavity-side issue. Because uneven cooling and hot runner temperature inconsistency tend to compound each other, this defect often has more to do with cooling system design than with the hot runner alone.
Likely causes: Uneven cooling allowing localized crystallization, resin sitting too long in a low-flow area of the manifold, or temperature running higher than intended in one zone, accelerating thermal degradation, are the most common contributors.
Troubleshooting approach: Identify whether haze appears consistently in the same preform location across multiple shots, which points toward a cooling or hot runner zone problem rather than a random process fluctuation. Reviewing actual residence time in the affected flow path, and confirming it matches the resin manufacturer's recommended limits, often reveals whether the hot runner system itself is the source.
Common Problem: Short Shots in Specific Cavities
A short shot affecting the same cavity or cavities repeatedly, rather than occurring randomly across the mould, usually points to a hot runner mould issue rather than a general process setting problem.
Likely causes: Partial blockage in a nozzle or gate, insufficient heat in that specific zone preventing resin from flowing properly, or a mechanical obstruction in the flow path are common causes.
Troubleshooting approach: Confirm the pattern is cavity-specific and repeatable before adjusting overall injection pressure or speed, since a global process change made to compensate for a localized hardware issue typically affects every other cavity that was already filling correctly.
Common Problem: Black Specks or Resin Degradation
Dark specks or streaks in finished preforms typically indicate resin degradation somewhere in the hot runner flow path, often in an area where material sits longer than the rest of the system.
Likely causes: Dead spots in manifold or nozzle design where resin can stagnate and degrade, excessive temperature in a localized zone, or contamination from a previous resin or colour run are the most frequent sources.
Troubleshooting approach: If the issue appears gradually after a colour or resin changeover, manifold cleaning is often the fix. If it persists after cleaning, the manifold's internal geometry may have a flow dead spot that requires design review rather than a process or cleaning adjustment.
A Practical Troubleshooting Approach
Effective troubleshooting on a hot runner PET preform mould generally follows the same sequence regardless of which specific defect is occurring:
-
Confirm the pattern first. Determine whether the issue affects specific cavities consistently, appears randomly, or correlates with a specific point in the production run, since each pattern points toward a different category of cause.
-
Verify instrumentation before adjusting settings. Thermocouple accuracy and actual versus displayed temperature should be confirmed before changing process parameters, since adjusting settings based on inaccurate data tends to introduce new problems.
-
Isolate hardware from process causes. A defect that's consistent and cavity-specific usually points to a hardware issue in the hot runner mould itself, while a defect that fluctuates across the whole mould more often points to a process or material variable.
-
Document findings before repairing. Recording what was actually observed, measured, and corrected makes future troubleshooting faster if the same issue recurs, and helps distinguish a one-off event from a recurring design limitation.
Common Mistakes When Troubleshooting Hot Runner Issues
-
Adjusting global process settings to compensate for a localized hardware problem, which often resolves the original issue only to introduce inconsistency elsewhere in the mould.
-
Assuming displayed temperature matches actual temperature, without verifying thermocouple accuracy first.
-
Treating recurring defects as isolated incidents, rather than tracking patterns that point to an underlying manifold or component design issue.
-
Skipping manifold inspection after a resin or colour changeover, when degradation-related defects appear.
-
Delaying root cause investigation by repeatedly replacing a worn component without identifying why it's wearing faster than expected a pattern that usually costs more over time than addressing it through proper maintenance planning.
Where This Fits with Dowell Moulds
Dowell Moulds designs hot runner PET preform moulds with manifold balance, cooling integration, and component serviceability considered from the original design stage, which reduces the likelihood of the recurring issues covered above. For manufacturers currently troubleshooting a production issue or evaluating a PET preform mould manufacturer on long-term reliability, our engineering team can review specific symptoms, and our spare parts support helps keep a mould running once a worn component is identified.
Final Takeaway
Most hot runner PET preform mould problems follow identifiable patterns once they're actually investigated systematically, rather than being random or unexplainable. Confirming whether an issue is cavity-specific or mould-wide, verifying instrumentation before adjusting settings, and tracking recurring defects back to their design-stage cause tends to resolve problems faster and more permanently than repeatedly adjusting process parameters to compensate for an underlying hardware issue.