
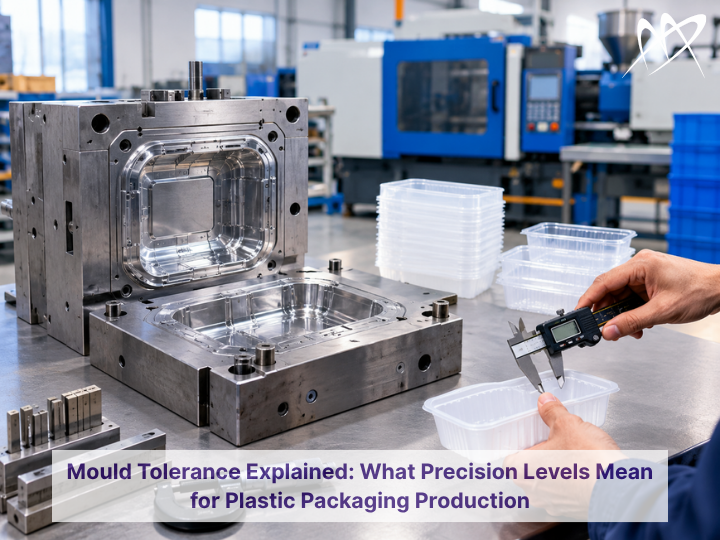
Mould tolerance is one of the least discussed specifications in a plastic packaging project, and one of the most consequential. It rarely gets the attention that cavitation count, cycle time, or material selection receive during initial planning, yet it directly determines whether a finished part seals, fits, and functions correctly once it leaves the mould.
The reason mould tolerance gets overlooked is simple: it sounds like a manufacturing detail rather than a business decision. In practice, it's closer to the second. How tightly a plastic mould tolerance is specified affects cost, machining time, and how reliably a component performs alongside other parts in a packaging line.
What Mould Tolerance Means
Mould tolerance is the permitted range of variation around a target dimension, expressed as a plus-or-minus value. A wall thickness specified at 1.20mm with a tolerance of ±0.05mm is considered acceptable anywhere between 1.15mm and 1.25mm.
Tolerance is not a general measure of mould quality. It's a functional agreement that defines the range within which a part still performs correctly for its intended use. A tighter tolerance is not inherently better it's appropriate only when the application genuinely requires that level of mould precision. Specifying unnecessarily tight tolerance adds machining time and cost without improving how the part actually performs.
Why Tolerance Carries More Weight in Plastic Packaging Mould Projects
Plastic packaging components typically function as part of a system rather than in isolation. A preform is blown into a bottle. A cap seals against a neck finish that may have been produced on a separate plastic packaging mould, sometimes by a different manufacturer. A closure applies torque consistently across a filling line operating at production speed.
Because these components interact with each other, a part can meet its own individual tolerance and still contribute to a functional failure once combined with another component. A cap and a bottle neck can each be within their respective tolerance ranges and still fail to seal properly if those ranges sit at opposite ends of what's acceptable.
This is also a common source of disagreement between suppliers in a packaging supply chain. Two manufacturers can each provide inspection reports showing compliance, yet the combined assembly still doesn't function as intended, because the tolerance ranges were never evaluated against how the parts are meant to interact. Establishing that alignment before production begins reduces the likelihood of this kind of dispute later.
This coordination becomes more important as a supply chain grows more fragmented. A packaging program sourcing preforms, caps, and labels from three separate manufacturers has three separate tolerance specifications that all need to reconcile with each other at the point of assembly. Without a shared reference point an agreed neck finish standard, for example, or a documented sealing surface tolerance each supplier can be technically correct in isolation while the finished package still underperforms.
How Injection Mould Tolerance Is Typically Specified
A mould drawing rarely applies a single tolerance value across every dimension, and it shouldn't. Sealing surfaces and thread engagement areas generally require tighter control than cosmetic or non-functional surfaces on the same part. Treating every dimension as equally critical increases cost without a corresponding functional benefit.
Cavity-to-cavity consistency is a separate consideration from individual mould dimensional accuracy. In a multi-cavity PET preform mould, each cavity may individually fall within tolerance while still varying enough from cavity to cavity to create inconsistency across a production batch. This becomes more significant as cavitation counts increase.
Tolerance specifications also need to account for process variation, not just the mould's baseline machining precision. Temperature, injection pressure, and cooling time all introduce their own variation during production. A mould that performs within tolerance during a short trial run may behave differently once it reaches thermal steady-state during a sustained, full-speed production run. A tolerance specification built only around ideal trial conditions tends to understate what actually happens once the mould is running continuously.
What Determines How Tight a Mould Can Hold
Achievable mould precision is not a claim a manufacturer makes independently of the build process it's a direct result of decisions made earlier in manufacturing.
Machining accuracy sets the upper limit. A cavity can only hold the tolerance it was originally machined to, which is why precision CNC and EDM machining has a significant effect on what a mould can realistically deliver.
Steel selection and heat treatment determine how long that precision is maintained. A mould built within tight tolerance initially can drift outside that range over months of production if the steel specification doesn't match the actual cycle count and production volume involved.
Cavitation adds a separate layer of difficulty. Higher-cavitation moulds require more surfaces to match each other consistently, not just the original design drawing, which makes tight cavity-to-cavity tolerance progressively harder to maintain as cavitation increases.
Part geometry also affects what's achievable. Thin walls and deep-draw features are more sensitive to small variations in fill and cooling than simpler geometries, leaving less margin for the natural shot-to-shot variation that occurs in any production run. A part with uniform wall thickness and minimal deep-draw detail gives a manufacturer more room to work within before a dimension approaches the edge of its tolerance range; a thin-walled preform with sharp internal transitions leaves considerably less room, which is one reason preform tooling is generally held to tighter and more carefully monitored tolerance than simpler packaging components.
Tighter Tolerance Is Not Automatically the Right Choice
A common assumption in mould specification is that requesting the tightest available tolerance is the safer decision. In most cases, this simply shifts cost and machining time onto dimensions that don't require that level of precision to function correctly.
A pharmaceutical closure that must seal reliably against contamination genuinely requires tight tolerance on its sealing surfaces. A cosmetic container with no sealing requirement does not need the same precision applied uniformly across every dimension, and specifying it that way adds expense without a corresponding functional gain.
The more useful approach is evaluating what each specific dimension requires based on its actual function, rather than defaulting to the tightest tolerance a manufacturer is capable of producing.
Where Tolerance Problems Typically Originate
Most tolerance-related issues trace back to unclear specification rather than poor machining.
Requesting "tight tolerance" without agreeing on a specific numerical range leaves the acceptable outcome open to interpretation between buyer and manufacturer. Applying uniform tolerance across every dimension, rather than reserving tighter control for functionally critical features, increases cost without improving performance. Overlooking cavity-to-cavity consistency in multi-cavity tooling allows individual cavities to pass inspection while the overall batch remains inconsistent. Assuming a tolerance figure discussed during quoting is automatically verified later, without confirming how and when that verification occurs, is a common gap between specification and actual production outcomes.
Confirming Tolerance Compliance in Precision Mould Manufacturing
A tolerance specification has limited value without a defined method for confirming a mould actually meets it. Coordinate measuring equipment is typically used to verify critical dimensions with a level of precision manual gauges cannot reliably provide, particularly on complex geometry such as neck finishes or thread profiles.
Statistical sampling across an extended production run provides a more accurate picture than measuring only the initial parts produced, since tolerance drift often becomes apparent only after a mould reaches thermal steady-state. Functional testing, separate from dimensional measurement, confirms actual performance a component that measures within tolerance but fails a torque or seal test indicates an interaction issue rather than a purely dimensional one.
This verification process connects directly to mould trial and validation, where tolerance compliance is tested under realistic production conditions rather than assessed from a limited number of early trial shots.
Final Takeaway
Mould tolerance determines whether packaging components function correctly once they interact with other parts in a production line, making it a specification with direct consequences rather than a background technical detail. Defining tolerance clearly, applying tight mould precision only where functionally necessary, and confirming compliance through structured trial data rather than assumption reduces the risk of failures that only become apparent after production is already underway.
Dowell Moulds applies this approach across its hot runner cap mould, preform mould, and closures tooling projects. Manufacturers evaluating tolerance requirements for a specific application can review our manufacturing capabilities or contact our engineering team to discuss project-specific specifications.